Comparing Cleanroom Wall Panel Cores: Rockwool, Aluminium Honeycomb, or PU?
Comparing Cleanroom Wall Panel Cores: Rockwool, Aluminium Honeycomb, or PU?
In high-purity manufacturing environments—from pharmaceutical and biotech to semiconductor fabrication—selecting appropriate cleanroom components is critical. The right wall system design directly impacts operational efficiency, product quality, and compliance with stringent industry standards. Among these, the choice between Rockwool™, aluminium honeycomb, and PU (typically polyurethane or polyisocyanurate) core materials represents a fundamental decision affecting both performance and cost.
This comprehensive comparison examines their suitability for different cleanroom classifications (ISO 14644-1 Class 3-8) and applications, validates performance against ISO 14644-4 specifications, and considers integration requirements for both wall panels and specialized cleanroom doors. Making an informed choice requires understanding how core characteristics align not just with your cleanliness requirements, but also with the unique demands of your operating environment.
2. Core Material Comparison Standards & Specifications
To evaluate cleanroom wall panel cores effectively, we must reference key industry standards that measure cleanliness, material performance, and contaminant control:
- ISO 14644-1: Governs cleanroom classifications from ISO Class 3 (extremely high purity) to ISO Class 8 (general). Higher numbers indicate greater particle counts allowed in the environment.
- ISO 14644-4: Defines airflow performance and requirements for room classification calculations, governing air changes per hour (ACPH) specifications.
- FDA cGMP (21 CFR Part 211): Applies to pharmaceutical operations, requiring “no accumulation of insoluble particles on surfaces.”
- EU GMP Annex 1: Provides guidelines for sterile and non-sterile manufacturing, detailing requirements for cleanroom construction materials.
3. Rockwool™ Core in Cleanroom Applications
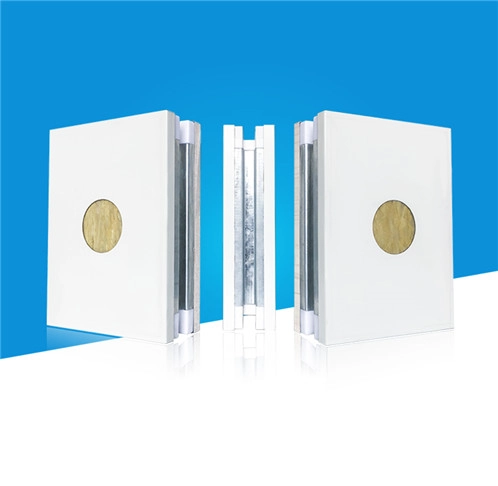
Fire Performance: Rockwool cores stand out with their exceptional fire resistance, meeting the highest A1 rating for surface combustion under ISO classification. This property is critical for facilities processing highly flammable materials or operating in fire-prone regions.
Structural Integrity: With compressive strength ratings of up to 100 kPa, Rockwool provides superior wall stiffness—a crucial factor in laboratories and pharmacies where wall stability prevents access door misalignment and maintains the integrity of vestibules and airlocks. This characteristic minimizes issues with our high-performance cleanroom doors that require precise seals.
Acoustic Properties: Sound transmission class (STC) ratings of up to 50 decibels make Rockwool ideal for environments requiring minimal reverberation—particularly important in labs and hospitals with high foot traffic and conversation levels.
Limitations: Heavier weight necessitates stronger anchoring systems compared to lightweight alternatives, potentially increasing overall structural complexity and installation costs.
4. Aluminium Honeycomb Core Performance Analysis
Optimal Lightweight Design: With core weights as low as 0.5 kg/m², aluminium honeycomb panels facilitate rapid deployment cleanroom construction—ideal for emergency containment or temporary sterile processing in pharmaceutical settings.
Barrier Efficiency: Providing excellent moisture resistance (up to 0.1% water absorption), these panels are suitable for high-humidity environments like those utilizing VHP sterilization common in ISO 7 pharmaceutical labs. However, they satisfy only basic particle barrier requirements without the fire resistance of Rockwool.
Mechanical Performance: Excellent resistance to point loads and warping enables construction of wider span walls—important when designing around our advanced modular wall panels and minimizing support structures between cleanroom entrances and interior spaces.
Limitations: Higher cost point-by-point compared to PU solutions but typically less insulating than premium Rockwool variants, making them less suitable for energy-intensive environments without supplementary thermal barriers.
5. Thermal Insulation Performance: PU Cores
Superior Thermal Resistance: PU/PIR foam offers lambda values as low as 0.022 W/m·K, making it the market leader for maintaining temperature stability in environments sensitive to thermal shifts or costly HVAC management.
Dimensional Stability: Excellent resistance to out-gassing ensures these panels maintain precise dimensions throughout long-term operation—an essential attribute in semiconductor manufacturing where panel distortion could impact wafer processing alignment and our specialized cleanroom door gap sealing.
Suitable Standards: Meets FDA cGMP requirements for surface cleanliness and smoothness. When properly formulated, PU cores often receive fire classification A2 or A3 further assisting compliance.
Installation & Lifespan: Their limited 5-year warranty period requires acknowledgment in total cost analysis, particularly in facilities with extended operational planning horizons compared to Rockwool years.
6. Selection Criteria & Application Tables
Choose the core material that best addresses your critical requirements:
| Critical Requirement | Optimal Core Material | Application Recommendations |
|---|---|---|
| Maximum Fire Resistance | Rockwool™ | Bio-pharma filling lines, sterile product processing, fire safety zones |
| Minimum Wall Weight | Aluminium Honeycomb | Mobile cleanroom enclosures, retrofit projects, space-constrained labs |
| Best Thermal Insulation | PU/PUR Core | Energy-intensive manufacturing, cold storage facilities, sterile fill/finish areas |
| Extreme Humidity Tolerance | Aluminium Honeycomb | Regions with high ambient moisture, facilities using steam sterilization |
| Sound Attenuation Needs | Rockwool™ | GMP-certified manufacturing, laboratory environments, clinical trial facilities |
Note: All materials must be properly integrated with appropriate seaming techniques and UV-cured silicone glazing compounds to maintain ISO Class compliance and GMP requirements at all seams and door interfaces.
7. Integration with Farclean’s Cleanroom Wall Panels and Door Systems
When comparing cores, don’t forget to consider compatibility with your overall cleanroom system:
- Seam Compatibility: Rockwool panels typically require specialized expoxy-based sealants, whereas aluminium honeycomb panels lend themselves to polyurethane glazing compounds. Our systems are designed to accommodate all three material types.
- Impact on Door Design: The thickness of each core affects our door unit design—from extended gasketing systems in Rockwool installations to compact, space-efficient designs for lightweight aluminium panels.
- Wall-to-Door Alignment: All our modular wall panels incorporate precise, kerf-free splicing to ensure perfect alignment with our heavy-duty interlocking cleanroom doors.
Request Your Custom Cleanroom Wall Core Analysis
Farclean provides complete turnkey cleanroom solutions—manufacturing ISO-certified modular wall panels, high-performance ceiling systems, and specialized cleanroom doors that support diverse core material applications. Our team can assist with every aspect, from material selection to validation:
Contact our engineering specialists to discuss your specific cleanroom requirements against ISO 14644-1, 14644-4, and regulatory compliance standards. We deliver factory-direct solutions that ensure optimal performance while controlling costs across all manufacturing sectors.