Downflow Weighing & Sampling Dispensing Booth Solutions — Complete Design, Installation & Commissioning
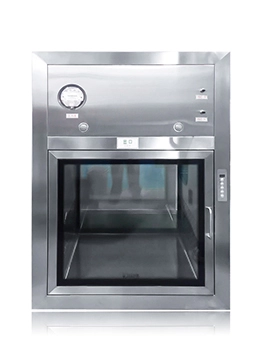
Farclean provides complete turnkey solutions for downflow weighing and sampling dispensing booths, ensuring precision, contamination control, and regulatory compliance in critical environments. Whether for pharmaceutical, biotech, or food processing applications, our integrated approach reduces project risks, accelerates installation, and guarantees full compliance with ISO and GMP standards, including the use of high-quality cleanroom doors and modular wall panels for optimal containment.
What Is a Downflow Weighing and Sampling Dispensing Booth Solution?
A downflow weighing and sampling dispensing booth solution is an integrated system designed to handle precise weighing operations and controlled dispensing within a contained environment. These booths feature specialized airflow patterns to minimize particle contamination, from initial setup to final validation. Working with Farclean means entrusting a single provider with engineering, material sourcing, construction, and regulatory documentation.
This ensures seamless operation with exceptional airflow control, meeting demanding ISO 14644-1 (ISO Class 3-8) requirements and other industry regulations.
Why Businesses Choose Turnkey Downflow Weighing & Dispensing Booth Solutions
- Single-source responsibility — one company manages design, cleanroom doors, modular wall panels, equipment installation, and certification.
- Shorter project delivery — streamlined coordination avoids delays common with multiple contractors.
- Cost transparency — clear project budgets with no hidden costs, ideal for downflow applications.
- Consistent quality — all components, including custom door systems and wall panels, adhere to uniform ISO and GMP standards.
- Enhanced safety — containing particulates during weighing and sampling; compliant with FDA cGMP (21 CFR Part 211) and EU GMP Annex 1 regulations.
Complete Downflow Weighing & Dispensing Booth Design & Engineering Services
At Farclean, our turnkey process starts with meticulous engineering based on your specific weighing needs, such as:
- Downflow classification: tailored airflow rates for ISO 5–7 classifications
- Sampling and dispensing protocols: optimized layout for user safety and efficiency
- HVAC load calculation: integrated systems with energy-saving features
- Modular wall panel customization: designed for flexible booth configurations
- Cleanroom door specifications: high-grade, airtight doors meeting particle containment standards
- Regulatory planning: ensuring alignment with ISO 14644-4 for booth validation
Our precise engineering minimizes errors in weighing and dispensing processes, bolstering compliance for standards like ISO 14644-1.
Key Components for Downflow Weighing & Dispensing Booths
A full turnkey booth includes essential elements optimized for downflow operations:
- Custom modular wall panels for booth enclosures and support structures
- Advanced cleanroom doors with sealing mechanisms for complete airflow control
- Specialized downflow systems: HEPA/ULPA filtration and controlled airflow units
- Integrated weighing scales and dispensing accessories
- Control panels and monitoring systems
- Built-in containment features compliant with FDA and EU GMP guidelines
Farclean ensures all components are seamlessly integrated, using durable modular wall panels and robust cleanroom doors for long-term reliability.
Professional Installation & Construction
Our construction process for downflow booths guarantees performance and safety:
- Structural framing and modular wall panel installation for steadfast enclosure
- Sealing and finishing to maintain airtight integrity, crucial for downflow containment
- HVAC ductwork and electrical controls for precise airflow management
- Installation of cleanroom doors and filtration systems
- Final booth setup, including user training and documentation preparation
Expert technicians follow strict protocols to validate airflows post-installation, ensuring performance under regulatory frameworks.
Testing, Commissioning & Validation
Before deployment, Farclean conducts thorough tests to confirm optimal performance for weighing applications:
- Air velocity and uniformity assessments for downflow patterns
- Particle count and filter leak testing using ISO 14644-1 standards
- Differential pressure verifications to maintain containment
- Calibration of weighing equipment to industry specs
- Temperature and humidity controls aligned with GMP requirements
- Comprehensive documentation for FDA and EU GMP audits
Receive detailed reports proving compliance for simplified regulatory reviews.
Applications for Downflow Weighing & Dispensing Booths
- Pharmaceutical dosing and compound preparation
- Biotech sampling and material handling
- Food industry precision weighing and packaging control
- Laboratory contamination-free dispensing operations
Advantages for Global Clients
Choosing Farclean for your downflow booth needs offers:
- Reduced costs through direct sourcing of premium materials, including durable modular wall panels and certified cleanroom doors
- Faster implementation with no delays from subcontractor issues
- Expert consultation for customized designs under ISO and FDA cGMP
- Ongoing support integrating with your compliance processes
Secure Your Turnkey Downflow Weighing Solution
Ready to enhance your precision operations? Farclean delivers end-to-end turnkey downflow weighing and sampling dispensing booth solutions, combining advanced engineering with proven regulatory compliance. From design and integration to installation and validation, we support industries worldwide.