How Customizable Sandwich Panels Accelerate Pharmaceutical Engineering Projects
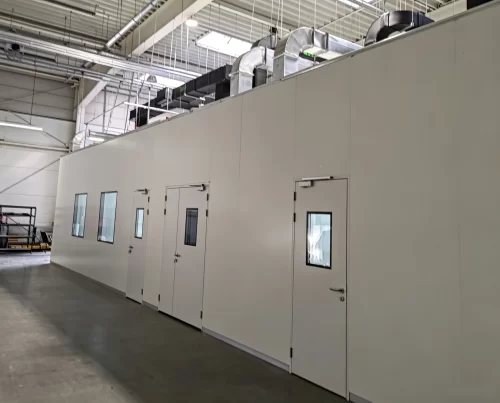
How Customizable Sandwich Panels Accelerate Pharmaceutical Engineering Projects
In today’s pharmaceutical industry, time-to-market is critical, and engineering projects must meet stringent regulatory standards like ISO 14644-1 (ISO Class 3-8), FDA cGMP (21 CFR Part 211), and EU GMP Annex 1. Modular and customizable sandwich panels—combining core insulation materials such as rockwool, aluminum honeycomb, or PU/PIR with durable facades—are increasingly being adopted to streamline cleanroom and isolation gowning room construction. These panels enable rapid assembly, reducing project timelines by 30-60% compared to traditional methods, while ensuring tight seals and contaminant control.
At Farclean, we specialize in turnkey cleanroom solutions, including high-performance modular wall panels with customizable core options for superior insulation, strength, and compliance. Our expertise extends to designing integrated cleanroom doors that automate pressure differentials and facilitate GMP adherence. This guide delves into how these panels accelerate pharmaceutical projects from design to operation.
1. Quick Overview: Customizable Sandwich Panels by ISO Cleanroom Classification
Cleanroom projects demand specific insulation and structural properties aligned with ISO 14644-1 standards. The core material of sandwich panels plays a vital role in achieving desired thermal performance and contaminant barrier integrity. Here’s how different core options adapt to ISO cleanroom classifications to speed up projects:
| Cleanroom Classification | Panel Core Material | Insulation Performance | Typical Application |
|---|---|---|---|
| ISO Class 8 | PU/PUR Foam Core | Excellent thermal R-value (up to 6.5 m²·K/W) | General pharmaceutical packaging, nutraceutical processing areas |
| ISO Class 7 | Rockwool Core | High fire resistance and moisture resistance (A1 rating) | Drug manufacturing lines, biologics production facilities |
| ISO Class 6 | Aluminum Honeycomb Core | Lightweight with high rigidity (low thermal conductivity) | Isolation gowning rooms, aseptic filling zones |
| ISO Class 5 & ISO 4+ | Hybrid Core with PU/PIR | Superior insulation combined with ease of cutting for clean seams | High-purity drug synthesis labs, semiconductor-grade sterile filtration units |
Note: Customization options include pre-finished surfaces compliant with GMP standards, allowing for quick integration into pharmaceutical projects.
2. Cost Component Breakdown: Optimizing Investment for Faster Project Delivery
To maximize the acceleration of pharmaceutical engineering, understanding where your investment in customizable sandwich panels goes is essential. Here’s how various components contribute to project speed and efficiency:
A. Core Materials and Insulation Systems (25% – 40% of Total Panel Cost)
The core of sandwich panels determines thermal efficiency, weight, and ease of installation, key factors in speeding up construction under ISO standards.
- PU/PUR Foam Core: Ideal for ISO Class 8 due to its high insulation value and fast installation. Reduces energy costs, aligning with facility expansions under EU GMP Annex 1.
- Rockwool Core: Mandatory for fire-safety-critical areas in ISO Class 7 and above. Provides A1 fire rating, meeting stringent GMP requirements for pharmaceutical storage.
- Aluminum Honeycomb Core: Perfect for rapid assembly in ISO Class 6 applications. Its light weight minimizes handling time and supports drop-ceiling integrations seamlessly.
B. Wall and Ceiling Integration (30% – 45% of Cost)
Modular wall panels with customizable cores can be snapped together or bolted for quick erection, reducing scaffold time.
- Insulation Focus: PU/PIR cores lower heating/cooling loads, accelerating energy payback in temperature-sensitive pharmaceutical storage rooms.
- Seamless Joints: Pre-fabricated panels with integrated gaskets minimize sealing gaps, enhancing air containment for projects adhering to 21 CFR Part 211.
C. Integrated Cleanroom Doors (15% – 25% of Cost)
Custom doors with acoustic seals and automated controls are crucial for differential pressure retention in pharmaceutical isolation zones.
- Options: Manual sliding doors for budget-sensitive ISO Class 8 rooms, or automated interlocking systems for sterile ISO Class 5 zones to prevent cross-contamination.
- Compliance: These doors often include materials like 304/316 stainless steel for VHP sterilization compatibility, as required by FDA cGMP standards.
D. Ancillary Systems (Flooring, Sealing, Automation) (10% – 20% of Cost)
Complete solutions include coved panels for flooring integration, reducing dirt-trapping surfaces and speeding up GMP validation cycles.
E. Engineering, Validation, and Turnkey Support (20% – 30% of Cost)
Our Farclean team designs panels for quick on-site assembly, cutting installation time. This includes IFE (Insitu Film Lamination) processes that meet ISO 14644-4 for better surface control.
3. Key Acceleration Factors Driving Pharmaceutical Project Success
Customizable sandwich panels can cut project timelines dramatically, especially in pharmacuetical settings where regulatory delays are costly. Key accelerants include:
- Modular Design and Rapid Assembly: Panels ship as complete sections with pre-cut edges, enabling 50% shorter installation periods compared to custom-built structures.
- Core Tailoring for Regulatory Compliance: Selecting cores based on application—e.g., rockwool for fire safety in ISO Class 6 labs—ensures quicker certifications under FDA cGMP and EU GMP guidelines.
- Reduced On-Site Labor and Waste: Factory-prepped panels minimize field errors, reducing risks of contamination during construction phases.
- Integration with Cleanroom Systems: Combined wall panels and door units with HEPA/ULPA filters (for filtration specs under ISO 14644-4) ensure faster startup for aseptic operations.
4. Customizable Sandwich Panels vs. Traditional Construction Methods
Traditional building techniques often involve lengthy modifications and higher error rates, delaying pharmaceutical projects. Here’s how our customizable panels outperform:
| Feature / Factor | Customizable Sandwich Panels | Traditional Construction |
|---|---|---|
| Assembly Time | Up to 50% faster due to standardized components | Slow, requiring on-site assembly and adjustments for walls, ceilings, leveling |
| Maintenance and Expansion | Hot-swappable panels for easy modifications and growth | Demolition needed for changes, leading to production downtime |
| GMP Compliance | Flush finishes and cleanable surfaces reduce validation time under ISO standards | Higher risk of particle shedding from drywall, needing extensive rework |
| Risk of Contamination | Factory-tested panels limit dust and particle emission during installation | High construction dust generates contaminated environments |
5. Strategies to Further Optimize Your Pharmaceutical Project Timeline
- Select the Right Core for the Application: Avoid over-engineering—use PU foam for warmer zones (ISO Class 8) to save costs and time, while reserving rockwool for critical fire areas.
- Adopt Pre-Integrated Solutions: Our Farclean sandwich panels come with factory-installed door frames and seals, eliminating on-site plumbing errors and reducing JIT challenges.
- Leverage Digital Design Tools: Use BIM software to simulate panel layouts, ensuring perfect fits and minimal rework for faster permit approvals.
Partner With Farclean for Accelerated Pharmaceutical Projects
Innovative solutions like customizable sandwich panels from Farclean empower pharmaceutical companies to meet tight deadlines while upholding ISO 14644-1, FDA cGMP, and EU GMP Annex 1 standards. Our modular wall panels and cleanroom doors are engineered for seamless integration into your engineering workflows, providing a reliable partner for turnkey cleanroom and pharmaceutical facility projects globally.
Contact our dedicated engineering group to explore how our advanced sandwich panel systems can drive efficiency, reduce costs, and ensure regulatory compliance for your next pharmaceutical venture.